Technologies
We provide development and manufacturing services for small-molecule and complex APIs, HP APIs, payloads and linkers for ADC, and oligonucleotides.
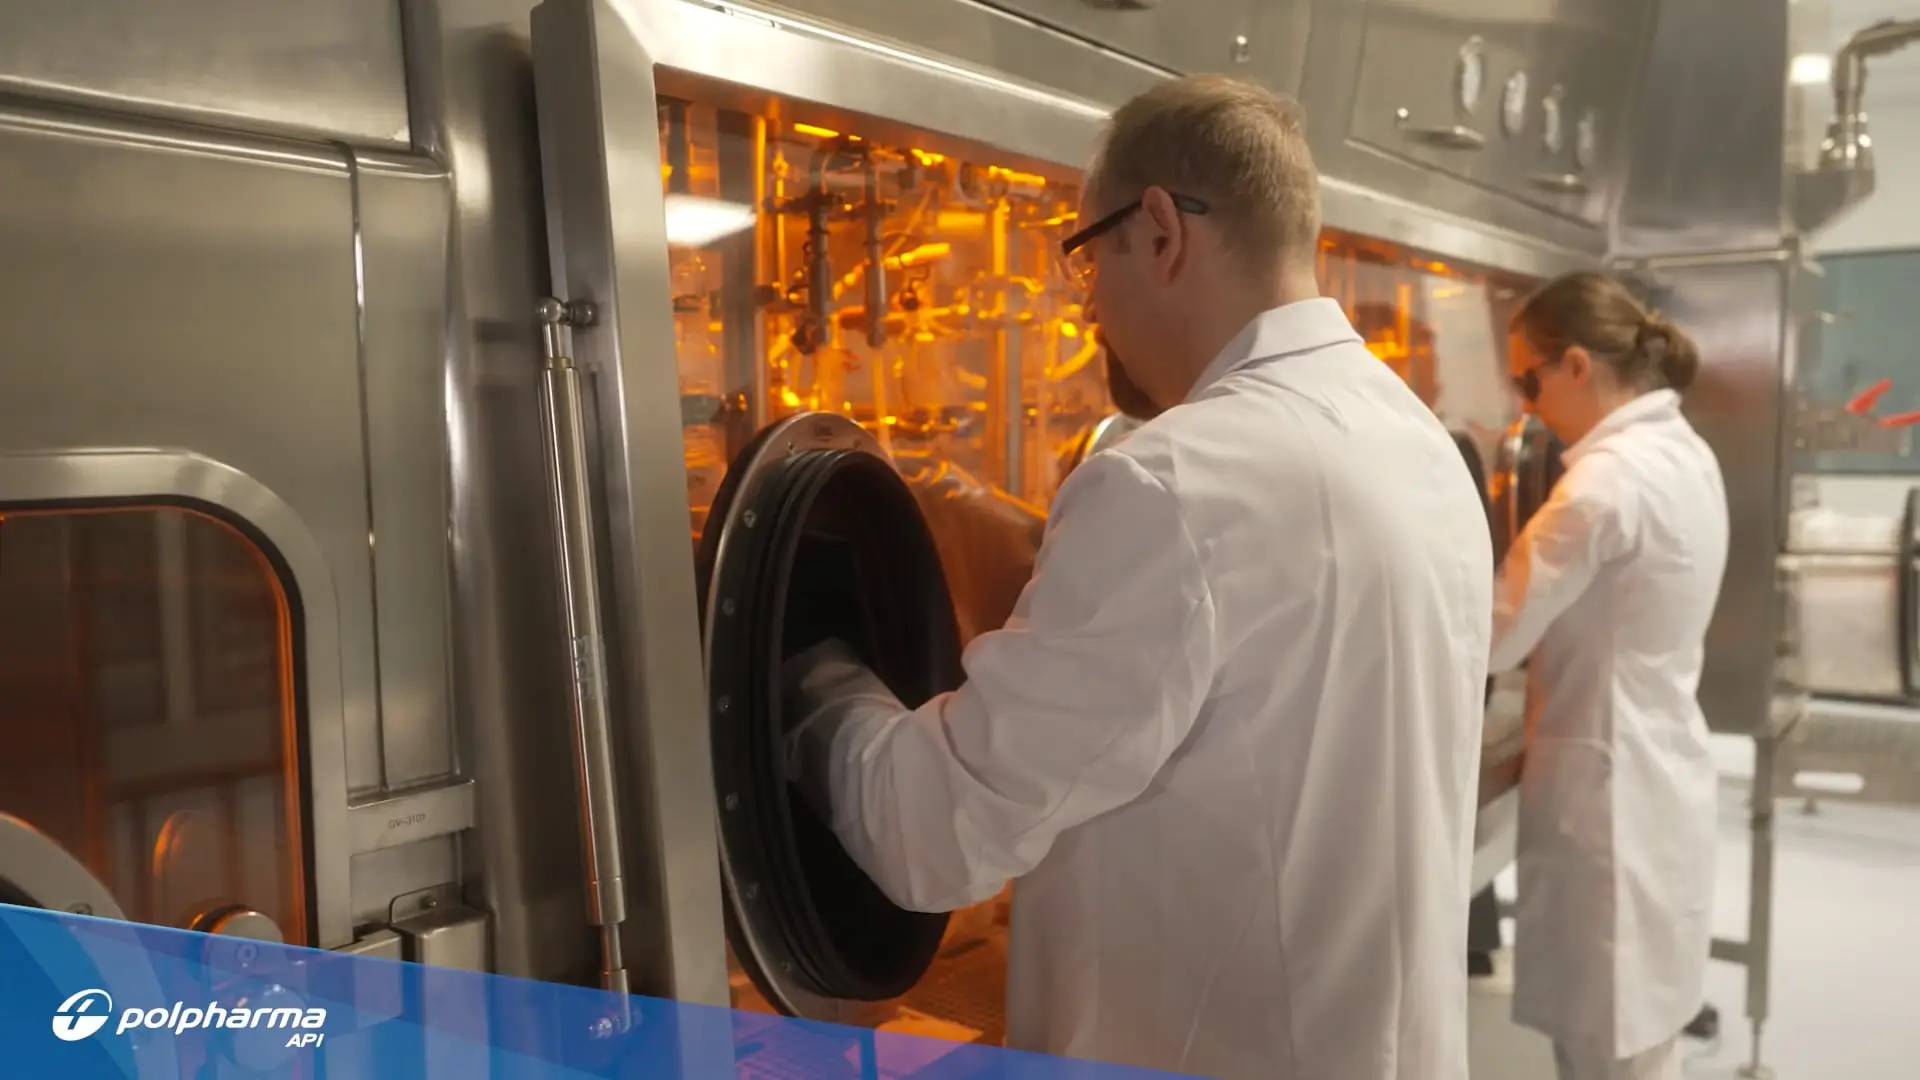
High Potent / ADC Payload-Linker
As an EU-based Contract Development and Manufacturing Organization (CDMO) and supplier of active pharmaceutical ingredients, we are advancing our technology capabilities with an Occupational Exposure Limit (OEL) as low as 10 ng/m³ (OEB 6).
Our capabilities enable GMP and FDA-approved kilo-scale production, offering batch sizes of up to 1.5 kg. This facility features dedicated Analytical Development Laboratories (ADL) and Process Development Laboratories (PDL) to ensure comprehensive support for development and production phases. The design incorporates state-of-the-art isolator technology to ensure the safety of both personnel and products, along with industry-standard secondary containment solutions integrated into the infrastructure.
We have secured future capacity expansion through both internal enhancements and external partnerships, with the goal of doubling our production capacity. This strategic approach enables us to support any business opportunities.
Building on our advanced high‑potency API capabilities, we support the development and manufacture of payloads and linker compounds for ADCs used in targeted therapies.
Our infrastructure and containment standards enable safe handling of highly potent, structurally complex molecules, while integrated process and analytical development ensures robust, scalable, and GMP‑compliant production.
By combining synthetic expertise with dedicated high‑potency laboratories and isolator‑based operations, we provide reliable support across development stages, from early process optimization to clinical and commercial supply, in line with stringent regulatory and quality requirements.
Product Class:
- OEL ≥ 10ng/m3
- OEB 5/6
Infrastructure:
- Process Development Laboratory (PDL)
- Analytical Development Laboratory (ADL) / QC
- Kilo-Lab
Targeted process outputs and regulatory compliance:
- PDL-scale up to 50g/batch, non-GMP area
- ADL-GMP/FDA compliant area
- Kilo-Lab-scale of 50g to 1,5kg/batch, GMP/FDA compliant area
Process Development Laboratory
- 4x Isolators (Dispensing unit, 2x Wet units and Dry unit)
- 2x Reactor 1000ml
- 2x Reactor 250ml
- 4x Reactor 100ml
- 2x Tray Dryer
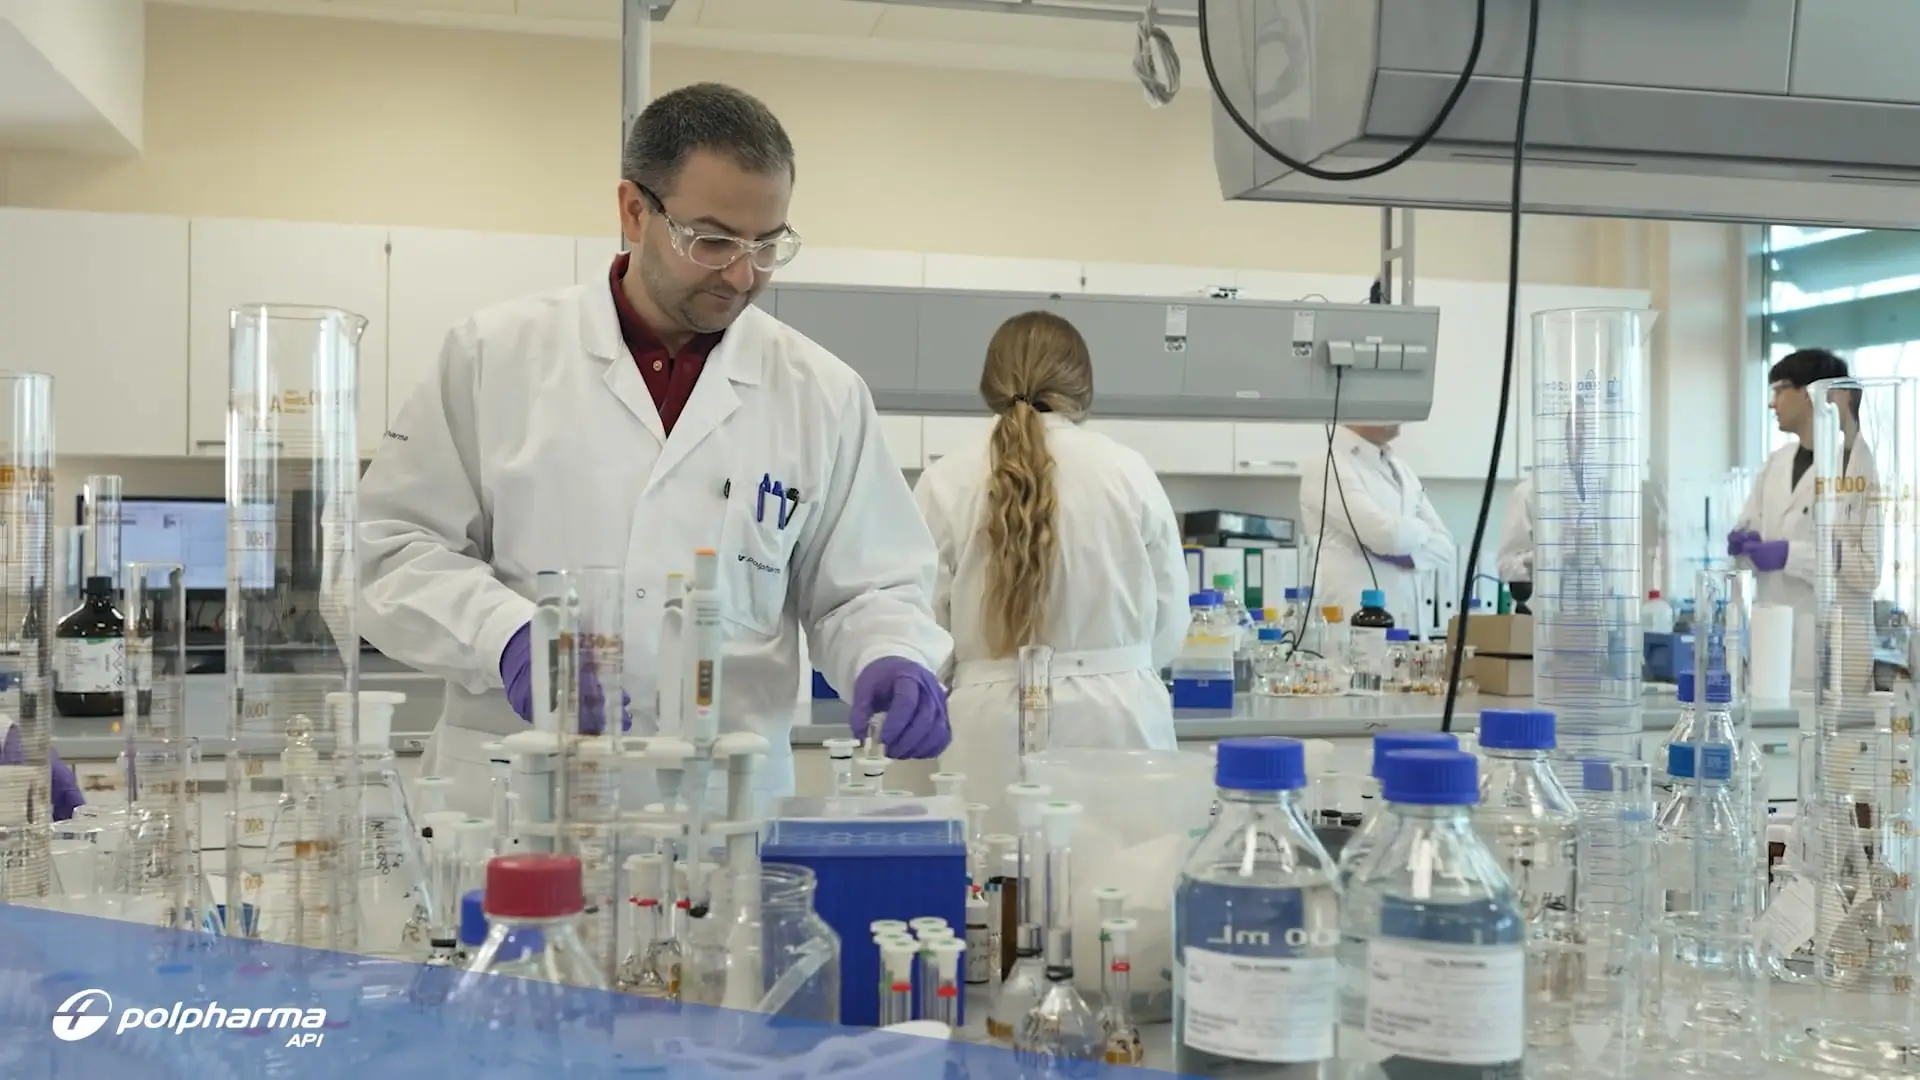
Analytical Development Laboratory + QC
- 5x Isolators
- 12x Fume Hoods
- 5x Ventilated Enclosures
- - HPLC with detectors: UV-Vis (PDA), RI
- - UPLC with detectors: UV-Vis (PDA), RI, MS, FLR
- - SFC (UPC2, Ultra-performance Supercritical Fluid Chromatography)
- - IC TGA
- - Titrators Malvern
- - IR, XRPD DSC
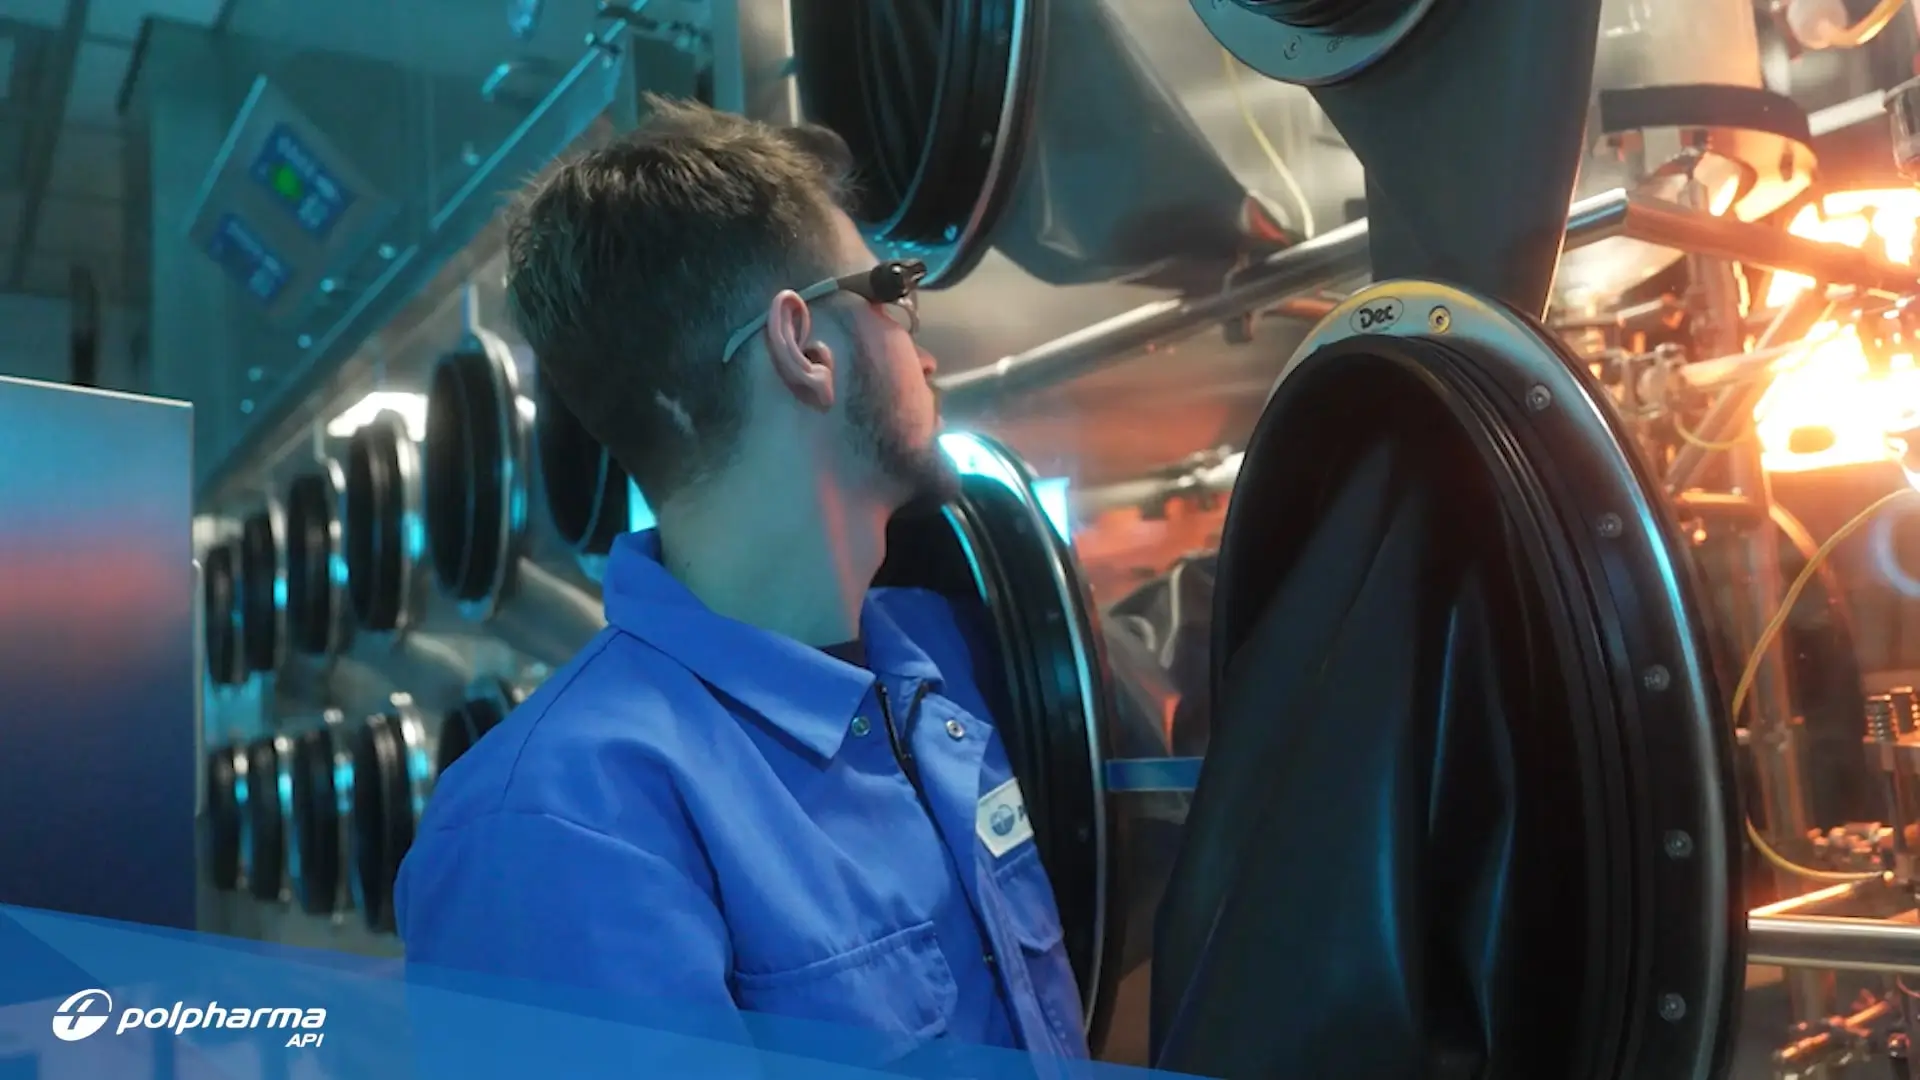

Oligonucleotides
At Polpharma API, we offer GMP-compliant oligonucleotide production with batch sizes up to 50 g, tailored to support clinical development and early commercial needs. Our facility integrates dedicated Analytical Development Laboratories (ADL) and Process Development Laboratories (PDL), ensuring robust support across all stages of development and manufacturing.
Upstream process development is powered by state-of-the-art Äkta oligosynt systems, enabling precise synthesis and scalable operations using FineLine 70 and AxiTide 50 synthetic columns. For purification, we deploy advanced in-house systems across both R&D and production scales — including Äkta pure 150, Äkta flux S, and the Hipersep Flowdrive Pilot with ProChrom 110 column — complemented by a customized TFF filtration system for reliable isolation, concentration, and diafiltration.
We also offer lyophilization scale-up process development, optimizing the final API structure for stability and performance. All downstream operations are conducted under sterile conditions, maintaining stringent microbiological standards and ensuring low endotoxin levels in the final API.
This integrated and strategic approach positions Polpharma API to effectively support clinical trials and accelerate the development of oligonucleotide-based therapies.
Upstream
Solid phase synthesis followed by cleavage & deprotection,
filtration and concentration.

Synthesizer
- Äkta oligosynt
- Scale <15 mmol
- FineLine 70, AxiTide 50 columns
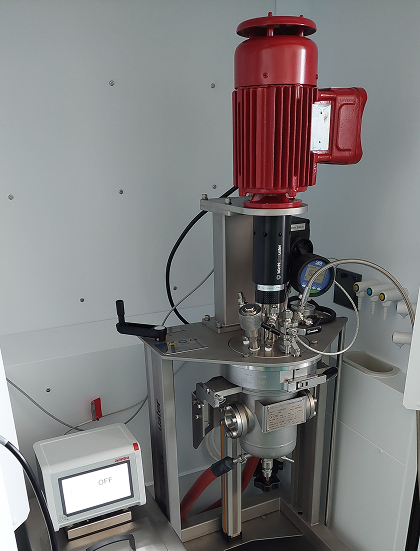
Ammonolysis Vessel
- High pressure stainless steel ammonolysis reactor
- Julabo dynamic temperature control system
- Capacity <2 L
Downstream
Tailor-made purification process with a sterile large-scale buffer preparation system (up to 100 L),
followed by ultrafiltration, diafiltration and endotoxin removal, lyophilization, weighing and packaging.
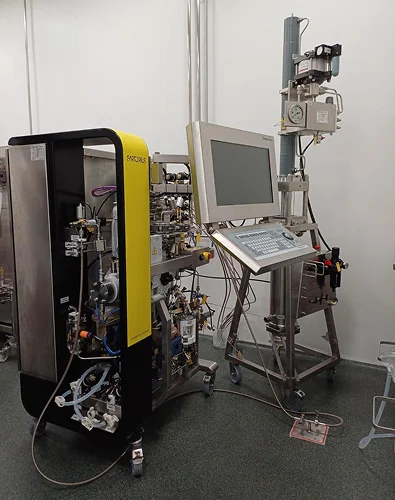
Chromatograph
- PROCHROM® HIPERSEP PILOT with Hipersep® Prochrom 110 Column
- Flow rate 6–90 L/h
- 1.5 L/min
- 100 bar

TFF system
- Customized TFF system
- Tank capacity <35 L
- Simultaneous production of water with reduced endotoxin level

Lyophilizer
- Epsilon 2-10D LSCplus
- area <1 m2
Cryogenic
Two cryogenic installations (pilot-scale 150 L and 400 L; commercial-scale 2,500 L and 6,300 L) operating below −90 °C, with experience in n-butyllithium and other organometallic reactions.

Pilot scale
- Reactor capacity range: 0.1 to 0.5 m3
- Operational temp. down to -90oC

Kilo-Lab
- Glass reactor: 35 Liters
- Operational temp. down to -90oC
- GMP conditions

Commercial scale
- 2 Hastelloy reactors (2 500l; 6 300l)
- 3 Glass-lined reactors (6 300l)
- Stainless Steel reactor (4 000l)
- Operational temp. down to -90oC
Capabilities

Equipment type
- Various types of reactors
- Columns
- Crystallizers
- Centrifuges
- Dryers
- Filter-dryers
- Mills
- Micronizers
- Lyophilizer
Operating ranges
- Temp. -90°C to +200°C
- Pressure -1 to +10 bars
- pH in the full range
Operating ranges
Pilot Plant
- Temp. -90°C to +200°C
- Pressure -1 to +10 bars
- pH in the full range

Equipment type

- Gringard reactions
- Catalyzed hydrogenation
- Metallation - Lithiation
- Superbases handling – alkyllithium, hydrides
- Lewis acid catalysis – boron/aluminum compounds

- Concentrated/gaseous ammonia handling
- Bromination/Chlorination
- Bisphosphonation
- Friedel-Crafts alkylation/acylation
- Inter- and intramolecular condensations
